Quality
Sterility is the standard
Quality in sterile compounding is not a department. It is how the room is built, how people are trained, and how every batch is checked before it leaves.
01
Controlled environments
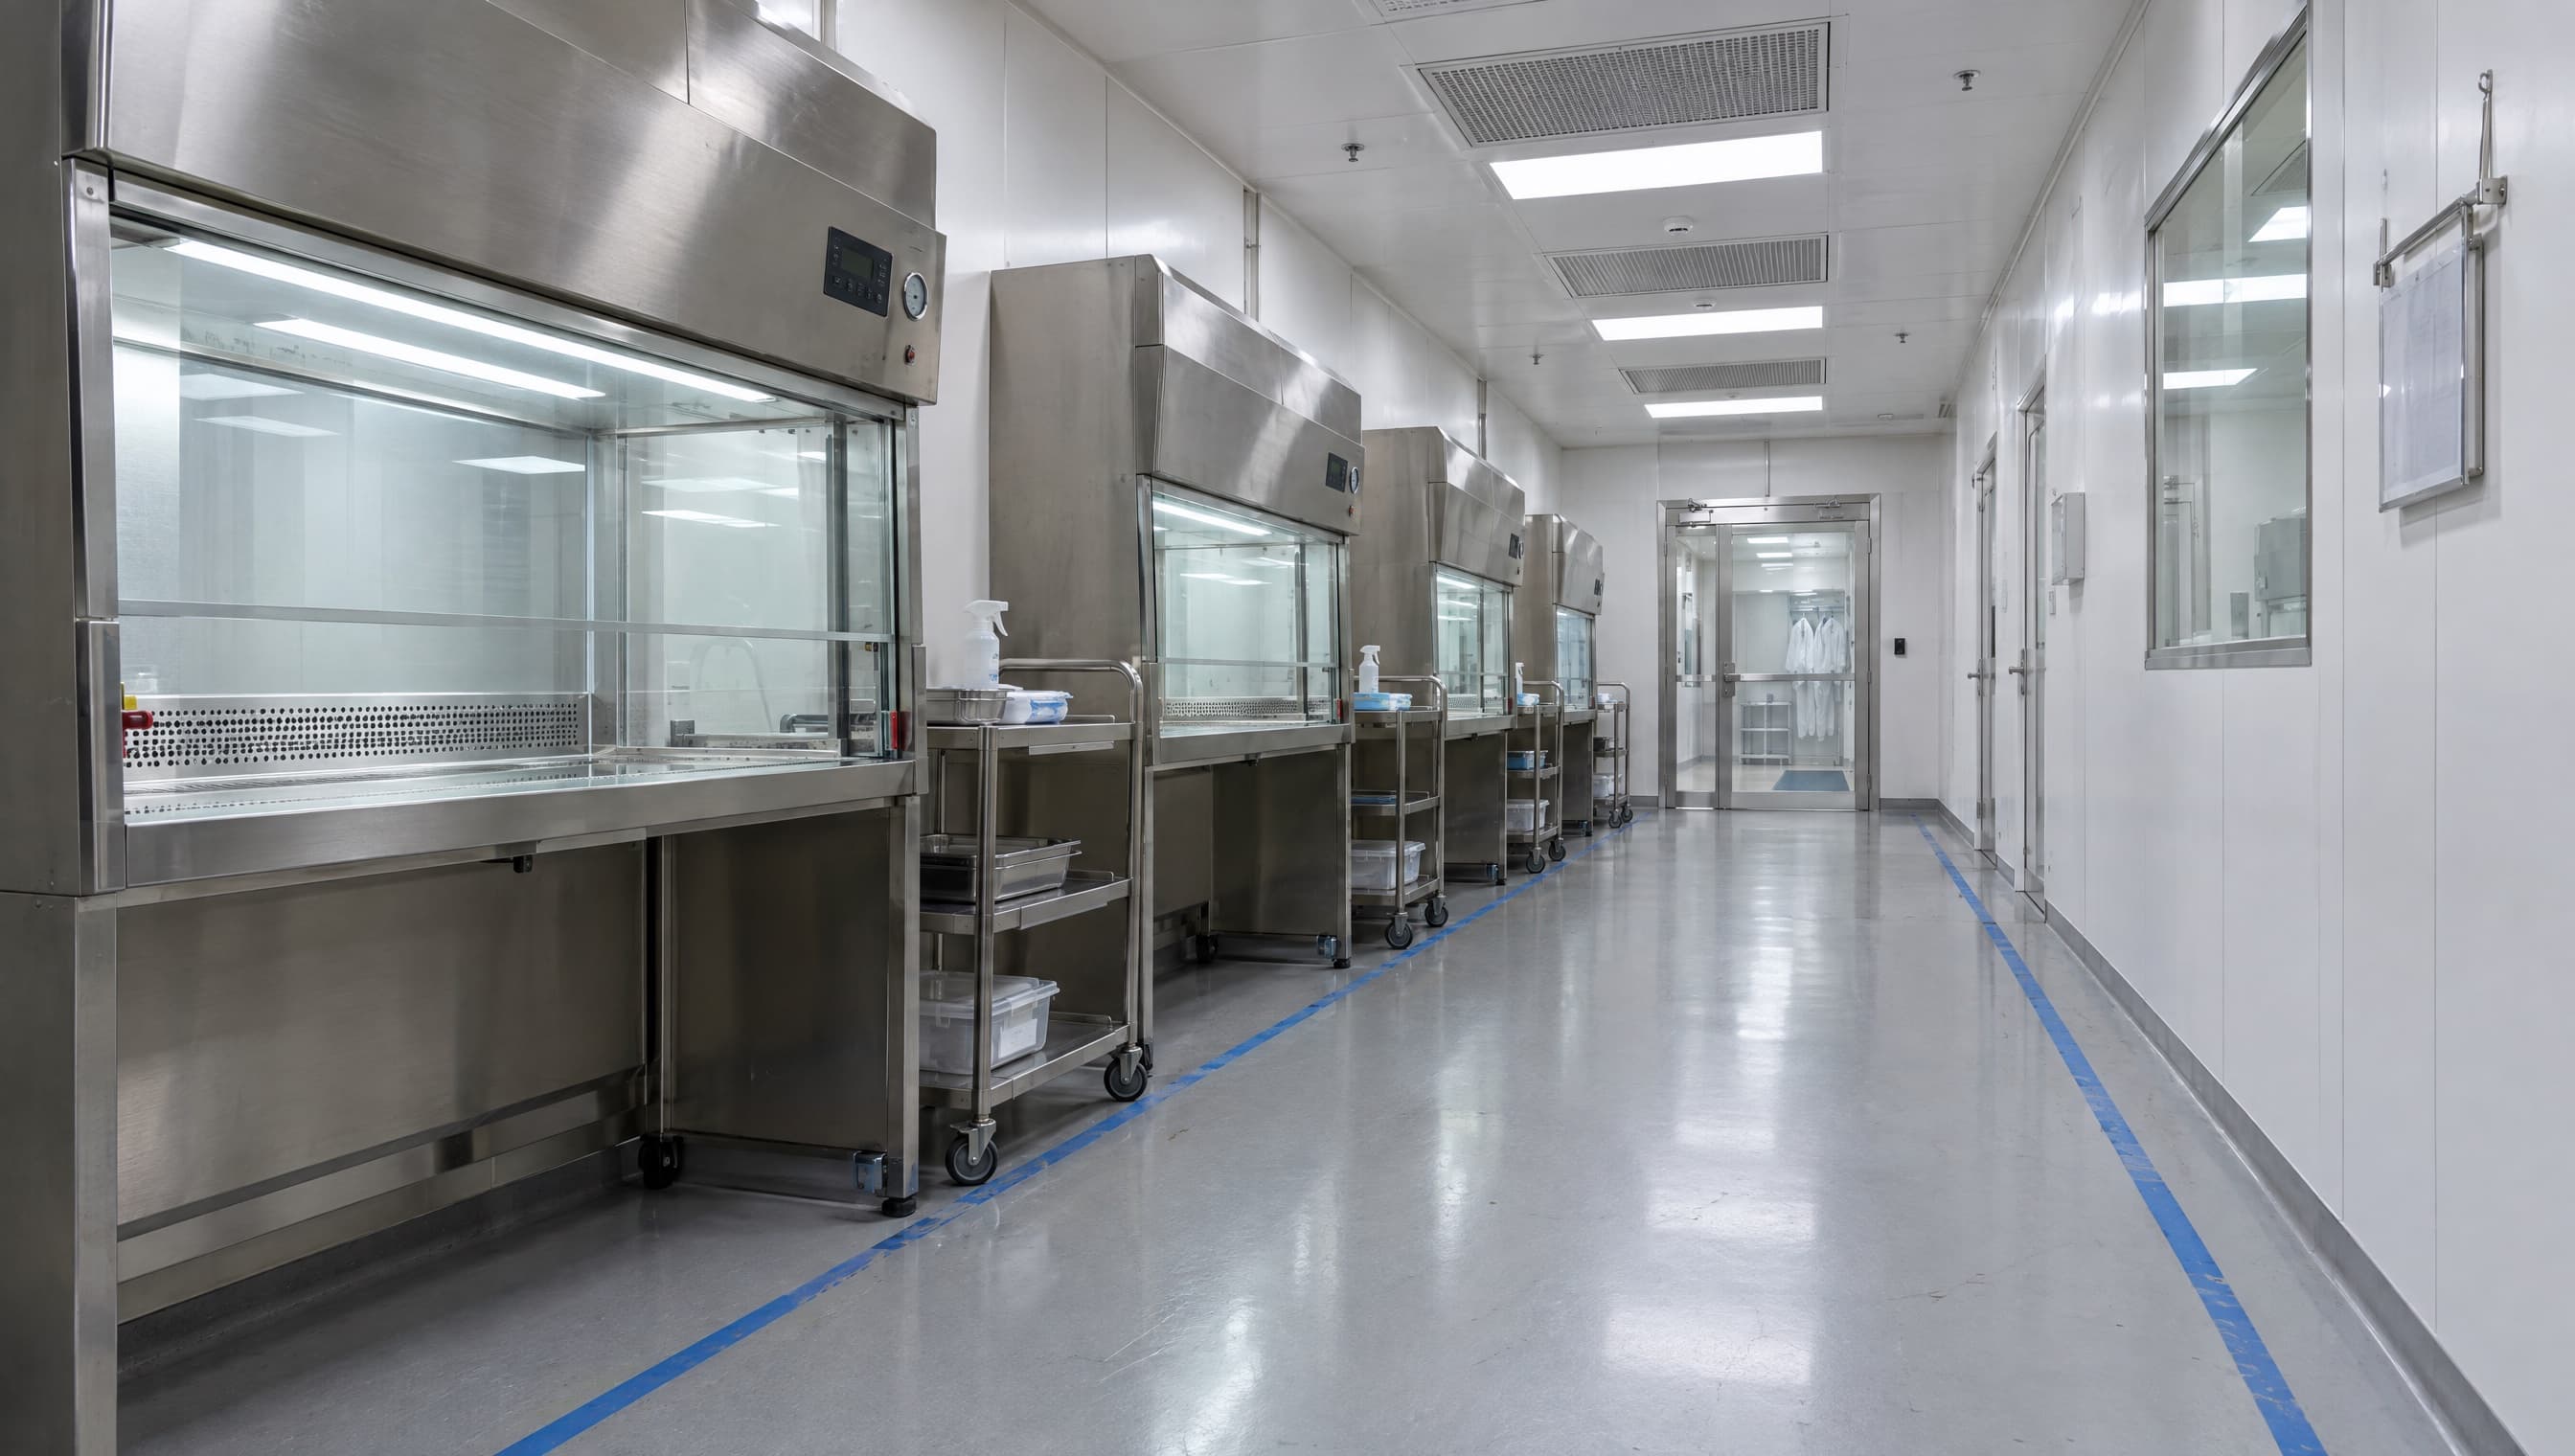
Sterile preparations are compounded inside ISO Class 5 primary engineering controls located within an ISO-classified cleanroom suite, with pressure, particle, and temperature monitoring.
02
Aseptic technique
Compounding staff are trained and routinely re-qualified in garbing, hand hygiene, and aseptic manipulation. Media-fill and gloved-fingertip testing are part of the routine, not a one-time event.
03
Testing & release
Batches follow a documented release process that can include sterility, endotoxin, and potency testing, alongside a final visual inspection of every unit before it ships.
04
Traceability
Lot numbers link each vial back to its ingredients, equipment, environment records, and the people who prepared and verified it.
05
Cold-chain shipping
Temperature-sensitive products ship in insulated packaging with cold packs, sized for transit time, to protect product integrity through delivery.
06
Continuous improvement
Environmental data, deviations, and customer feedback feed a quality program that is reviewed on a regular cadence and improved over time.
See the formulary and the states we ship to.
Final inspection
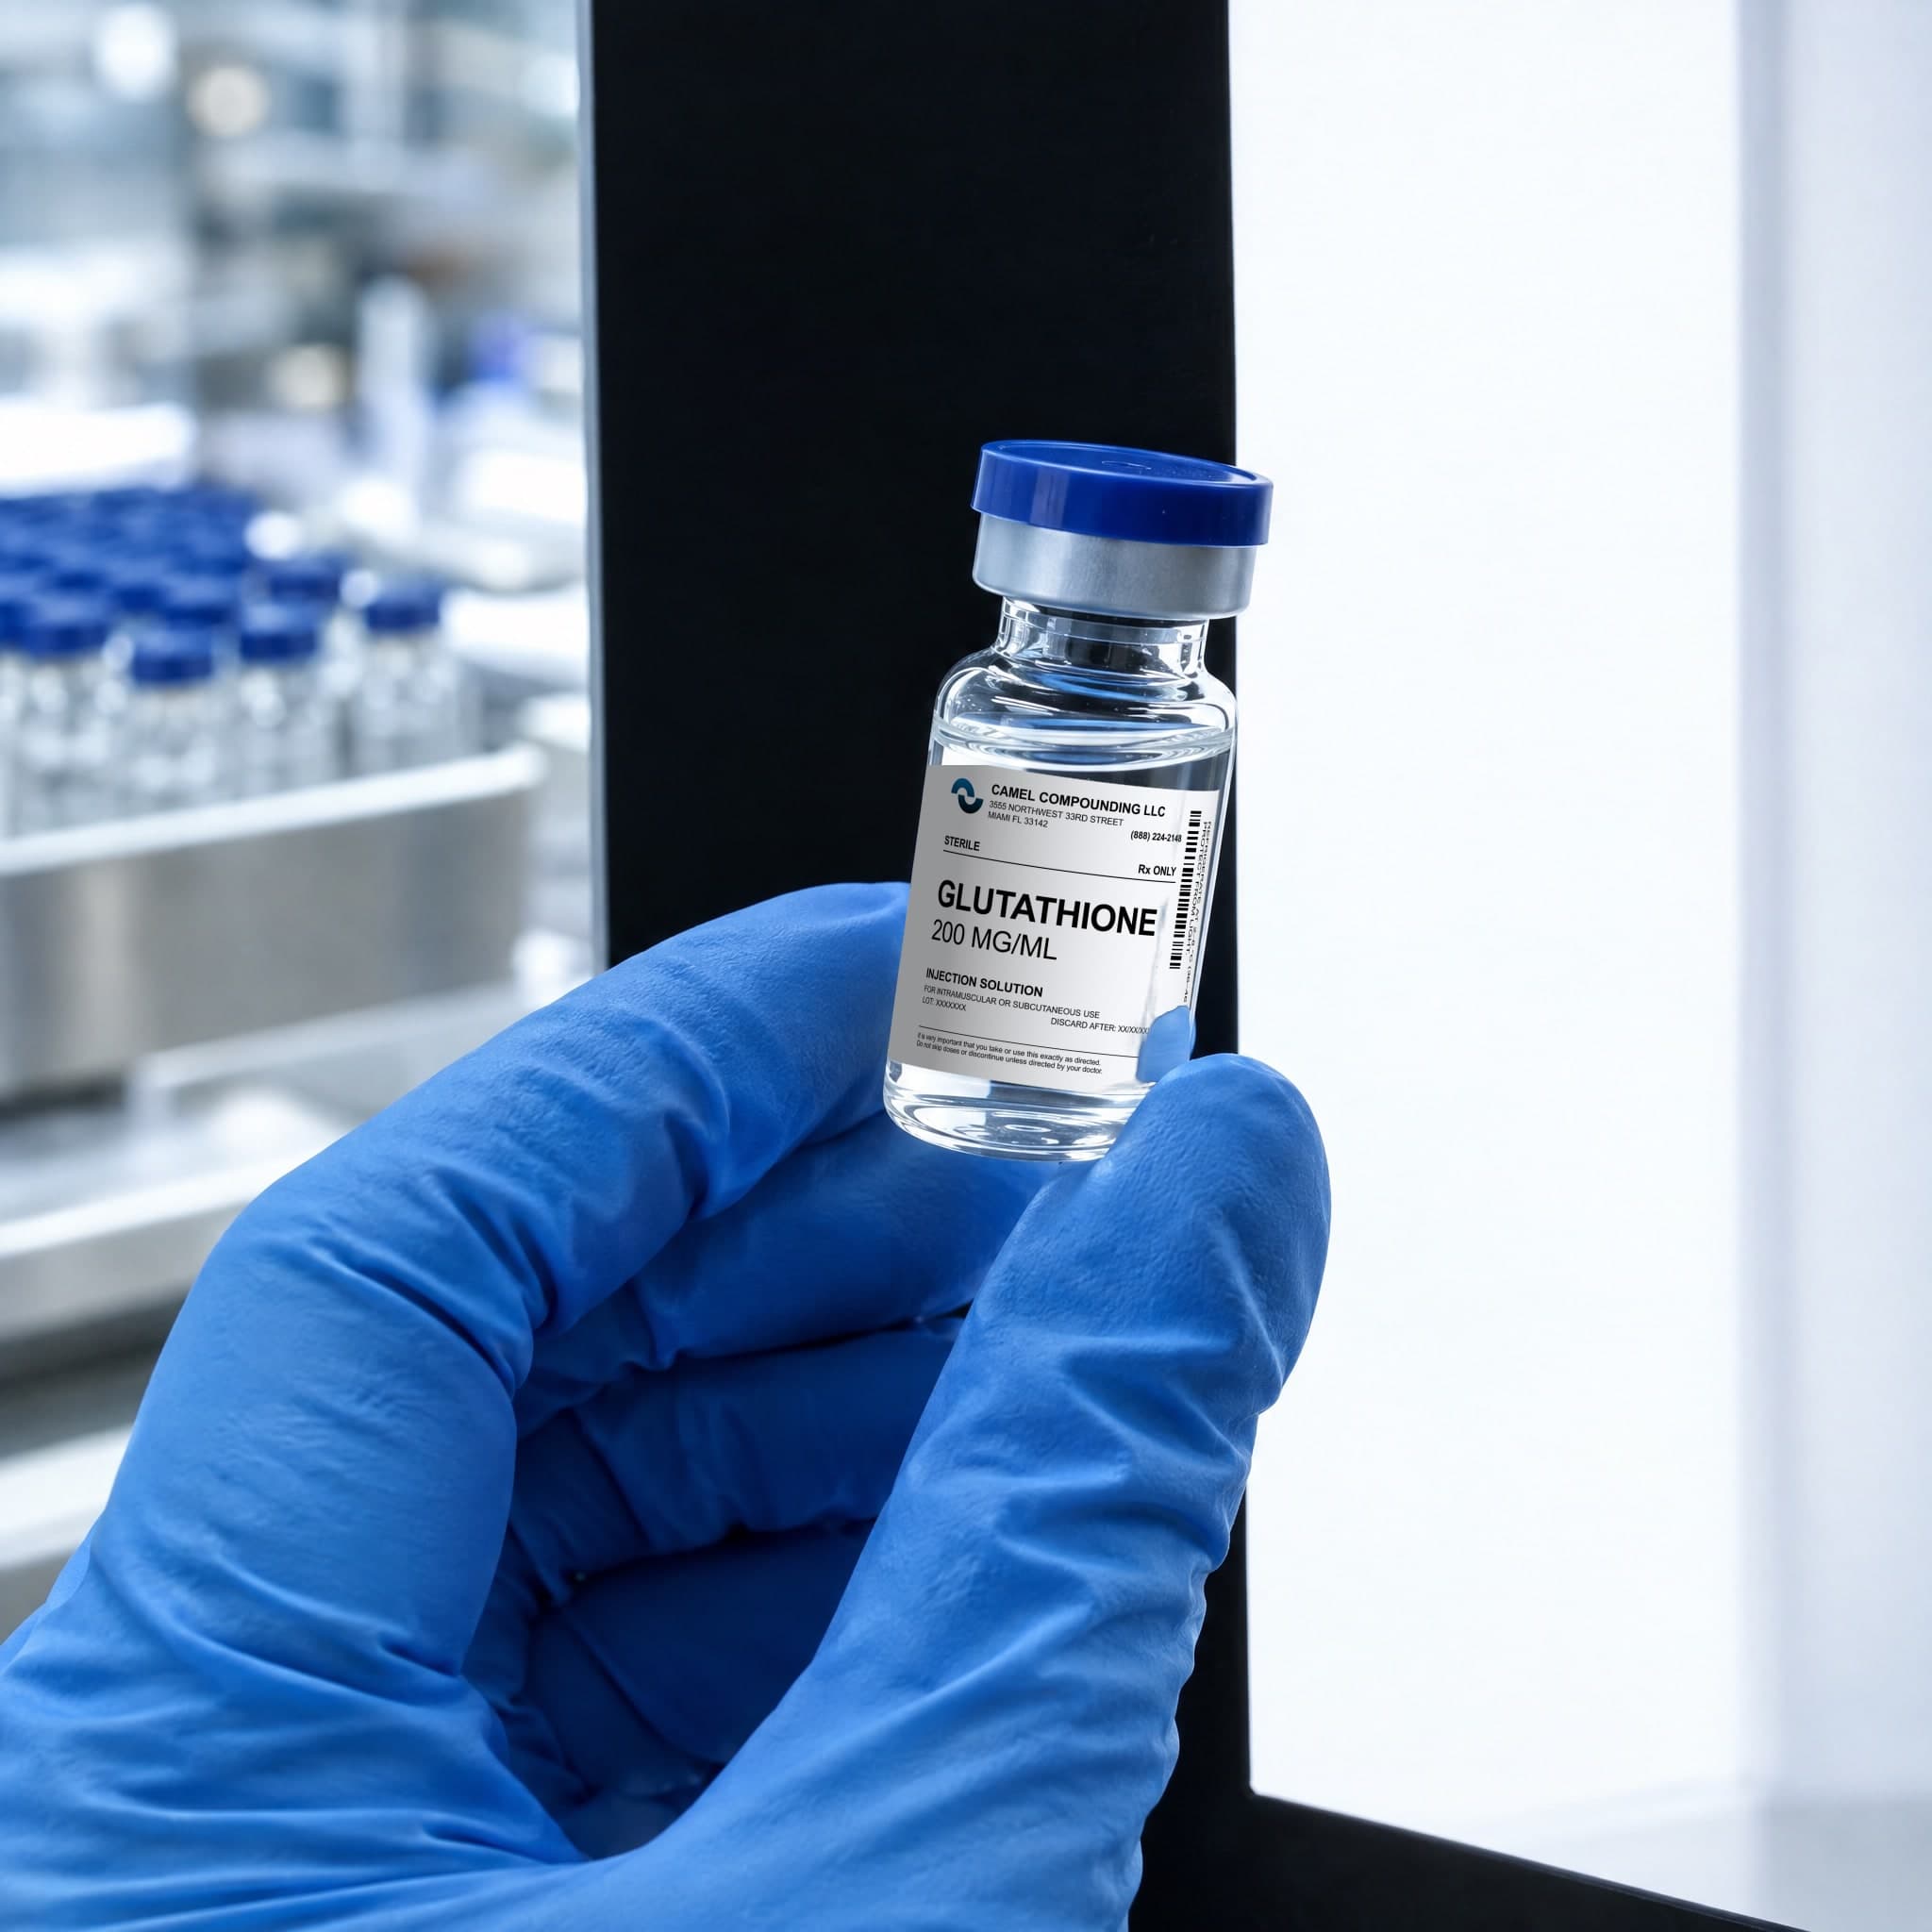
If it isn’t right, it doesn’t ship.
Every unit is inspected before release. Anything found outside specification is quarantined and investigated, and it is not released. It’s the simplest rule we have.